US Brewing Enzymes Market: Sourcing Guide for Breweries, Distributors and Formulators
How US breweries, distributors and formulators source brewing enzymes in bulk: demand drivers, key enzyme classes, supplier qualification and how to request a quote.
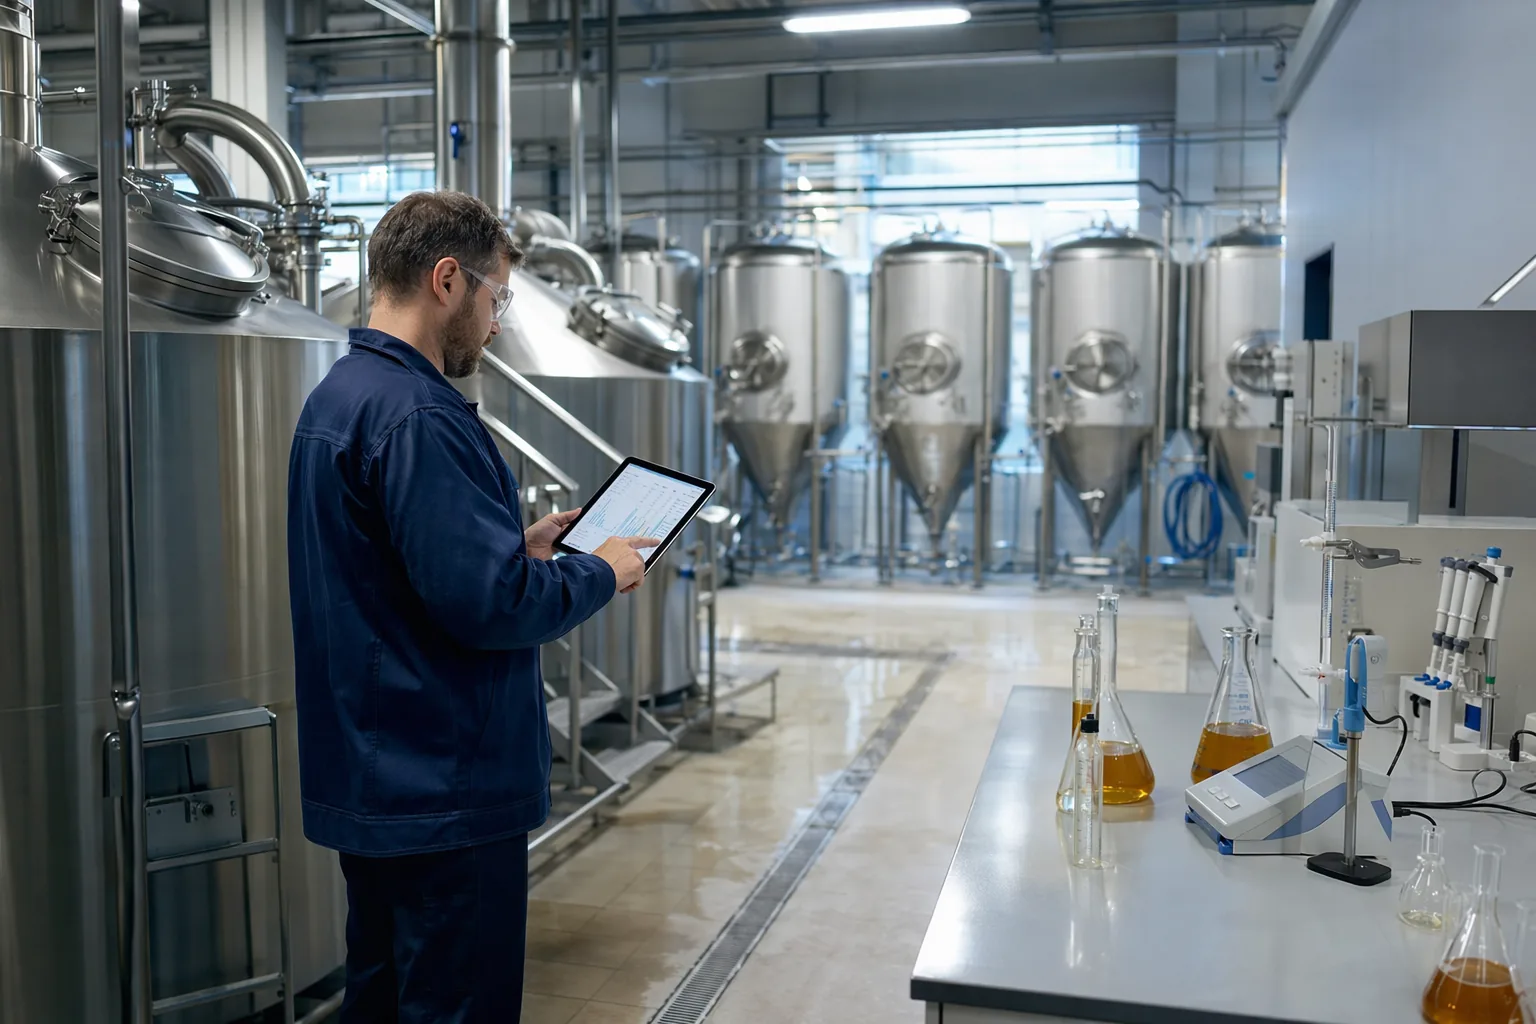
For breweries, malt houses, distillers and the distributors who supply them, enzyme selection is a process and purchasing decision. This guide explains how to evaluate brewing enzymes for yield, filtration, attenuation, clarity and cost-in-use, and how to turn market trends into a supplier shortlist.
Supply is liquid or powder in 25 kg drums or 200 L barrels, minimum order 25 kg, quoted per order. To request a quote, send the product or application, the quantity and the destination through the inquiry form.
Market Context for Brewing Enzyme Buyers
The us brewing enzymes market reflects a broader shift toward controlled, data-driven brewing operations. Rather than treating enzymes as commodity processing aids, breweries increasingly evaluate them against wort yield, viscosity reduction, fermentability, chill haze risk, filtration rate, and tank utilization. This mirrors wider brewing enzymes market trends seen in craft, regional, and large-scale production, where raw material variation and sustainability targets influence process design. Buyers comparing the global brewing enzymes market, african brewing enzymes market, and U.S. demand should avoid relying only on headline brewing enzymes market size or brewing enzymes market revenue estimates. Practical value depends on local malt quality, adjunct level, brewhouse configuration, and final beer specification. A strong brewing enzymes market analysis should connect enzyme functionality to measurable operating outcomes, not just brewing enzymes market share.
Use enzymes to manage raw material variability and process bottlenecks. • Benchmark suppliers by technical support, documentation, and batch consistency. • Separate market opportunity from plant-specific value creation.
Market Trends That Shape Buying Decisions
Current brewing enzymes market trends are shaped by raw material volatility, high-gravity brewing, low-alcohol and no-alcohol product development, faster clarification targets, and demand for consistent output across distributed production sites. The global brewing enzymes market is also influenced by breweries seeking local grain utilization, including sorghum, cassava, maize, and other adjuncts that require more deliberate enzyme programs. In the US brewing enzymes market, craft and regional brewers look for flexible enzymes that can solve hazy filtration, stuck mash, or attenuation variation without changing brand character. In the African brewing enzymes market, practical buying criteria may include performance with local grains, robust logistics, and cost-in-use under variable raw material quality. Buyers should turn these trends into test plans, specifications, and supplier scorecards.
Use market insight to shortlist enzyme classes, not to skip trials. • Validate regional raw materials under local water and mash conditions. • Reassess enzymes when recipes, adjuncts, or equipment change.
Key Enzyme Functions in Brewing
Brewing enzymes are selected according to the substrate and the process limitation. Alpha-amylase reduces starch viscosity during liquefaction or high-adjunct mashing, at conditions that depend on the formulation and are stated on the TDS. Glucoamylase brewing applications increase fermentable glucose for high-attenuation beers, low-carbohydrate styles or distilling wash, before fermentation or under supplier-approved conditions. Beta-glucanase lowers wort viscosity and improves lautering when barley, wheat, rye, or undermodified malt creates high beta-glucan levels. Proteases can support FAN development but must be controlled to avoid foam and body impacts. A beer clarification enzyme, such as a haze-reduction enzyme, is chosen for stability goals and must be validated against flavor, foam, and shelf-life expectations.
Alpha-amylase: starch thinning and liquefaction support. • Glucoamylase: higher fermentability and attenuation control. • Beta-glucanase: viscosity reduction and faster separation. • Protease: FAN adjustment and protein modification. • Clarification enzyme: haze management and filtration support.
Process Conditions and Dosage Planning
Dosage should start from the supplier TDS and then be optimized by pilot validation. The correct dosage depends on enzyme activity, substrate load, contact time, temperature, pH, calcium level and desired endpoint. For mash applications, confirm whether the enzyme is dosed into mash-in, cereal cooker, main mash, or conditioning tank. For beer clarification enzyme use, verify the correct stage, mixing intensity, residence time, and whether heat or filtration later inactivates or removes the enzyme. pH should be checked with calibrated meters, and temperature should be monitored at the point of addition rather than only at the vessel jacket. Overdosing can increase cost, create over-attenuation, affect mouthfeel, or complicate label and process declarations.
Begin with supplier-recommended dosage, then bracket trials above and below. • Track pH, temperature, time, and substrate concentration for every run. • Confirm inactivation, carryover, and compatibility with downstream steps.
Pilot Validation and QC Checks
A disciplined pilot program reduces scale-up risk and supports procurement decisions. Run a control batch without enzyme, a recommended-dose batch, and at least one reduced or increased dose batch. Measure extract recovery, iodine conversion, wort viscosity, beta-glucan level where relevant, turbidity, FAN, fermentability, apparent attenuation, filtration differential pressure, dissolved oxygen, and sensory impact. For glucoamylase brewing trials, compare real degree of fermentation, residual carbohydrate profile, alcohol yield, and endpoint gravity. For clarification trials, evaluate chill haze, forced aging stability, foam retention, and any flavor deviation. Documentation should include lot number, COA, TDS, SDS, storage history, addition point, and operator observations. Scale-up should be approved only when pilot data show repeatable gains under realistic raw material and production conditions.
Use side-by-side controls instead of relying on single-batch impressions. • Define pass/fail criteria before trialing the enzyme. • Retain samples for stability and sensory comparison.
Supplier Qualification and Cost-in-Use
Industrial buyers should qualify brewing enzyme suppliers through documentation, technical capability, and supply reliability. Request current COA for each lot, TDS for activity and handling guidance, SDS for safety controls, allergen or regulatory statements when relevant, and storage and shelf-life recommendations. Avoid purchasing only on price per kilogram; enzyme activity, liquid versus powder form, cold-chain needs, dosing accuracy, and plant losses can change the real cost. A practical cost-in-use model should include enzyme cost per hectoliter, extract gain, reduced lauter or filtration time, tank occupancy, energy use, waste reduction, and product consistency. Supplier qualification should also review change-control communication, lead times, packaging integrity, and access to application specialists who understand brewing, winemaking, and distilling operations.
Compare delivered activity, not only package price. • Require COA/TDS/SDS before production approval. • Build cost-in-use models using plant data and validated KPIs. • Confirm supplier support for troubleshooting and scale-up.
Technical Buying Checklist
Buyer Questions
Start with process needs rather than market headlines. Define whether the goal is faster lautering, better attenuation, improved clarity, adjunct flexibility, or yield improvement. Then compare suppliers by enzyme activity, documentation, technical support, lot consistency, lead time, and pilot trial results. Brewing enzymes market size and revenue data can show demand direction, but plant-specific cost-in-use determines the real purchasing decision.
Use a controlled design with at least one no-enzyme control, one supplier-recommended dosage, and one alternate dosage. Keep grist, mash schedule, water chemistry, yeast, and filtration settings consistent. Measure extract, viscosity, turbidity, FAN, attenuation, filtration time, and sensory results. Record pH, temperature, addition point, enzyme lot, and contact time so successful results can be repeated at production scale.
Request a COA for batch-specific quality attributes, a TDS for activity, dosage, conditions, and handling, and an SDS for safe storage and workplace controls. Buyers may also need lot traceability, shelf-life guidance, storage temperature recommendations, and relevant regulatory or allergen statements. Documentation should be reviewed before pilot work and again before approving routine production use.
Glucoamylase hydrolyzes dextrins into fermentable glucose, supporting higher attenuation, low-carbohydrate beer targets, or improved alcohol yield in distilling wash. It is usually evaluated around mildly acidic pH and moderate temperatures, subject to the product TDS. Buyers should monitor endpoint gravity, alcohol yield, residual carbohydrate profile, flavor, and over-attenuation risk before adopting glucoamylase brewing use at scale.
Cost-in-use depends on dosage, enzyme activity, addition stage, residence time, mixing, reduction in filtration load, tank turnaround, product losses, and stability performance. A cheaper enzyme may cost more if it requires higher dosage or causes inconsistent clarification. Validate with turbidity, chill haze, filtration pressure, foam, sensory, and shelf-life testing before selecting a routine production supplier.
Brewing & Winemaking Enzymes for Research & Industry
Need Brewing & Winemaking Enzymes for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
How should a brewery evaluate the us brewing enzymes market before purchasing?
Start with process needs rather than market headlines. Define whether the goal is faster lautering, better attenuation, improved clarity, adjunct flexibility, or yield improvement. Then compare suppliers by enzyme activity, documentation, technical support, lot consistency, lead time, and pilot trial results. Brewing enzymes market size and revenue data can show demand direction, but plant-specific cost-in-use determines the real purchasing decision.
What is a practical pilot trial design for brewing enzymes?
Use a controlled design with at least one no-enzyme control, one supplier-recommended dosage, and one alternate dosage. Keep grist, mash schedule, water chemistry, yeast, and filtration settings consistent. Measure extract, viscosity, turbidity, FAN, attenuation, filtration time, and sensory results. Record pH, temperature, addition point, enzyme lot, and contact time so successful results can be repeated at production scale.
What documents should industrial buyers request from an enzyme supplier?
Request a COA for batch-specific quality attributes, a TDS for activity, dosage, conditions, and handling, and an SDS for safe storage and workplace controls. Buyers may also need lot traceability, shelf-life guidance, storage temperature recommendations, and relevant regulatory or allergen statements. Documentation should be reviewed before pilot work and again before approving routine production use.
How is glucoamylase used in brewing and distilling applications?
Glucoamylase hydrolyzes dextrins into fermentable glucose, supporting higher attenuation, low-carbohydrate beer targets, or improved alcohol yield in distilling wash. It is usually evaluated around mildly acidic pH and moderate temperatures, subject to the product TDS. Buyers should monitor endpoint gravity, alcohol yield, residual carbohydrate profile, flavor, and over-attenuation risk before adopting glucoamylase brewing use at scale.
What affects the cost-in-use of a beer clarification enzyme?
Cost-in-use depends on dosage, enzyme activity, addition stage, residence time, mixing, reduction in filtration load, tank turnaround, product losses, and stability performance. A cheaper enzyme may cost more if it requires higher dosage or causes inconsistent clarification. Validate with turbidity, chill haze, filtration pressure, foam, sensory, and shelf-life testing before selecting a routine production supplier.
What are the most common reasons brewing enzymes fail in production?
Common causes include dosing on the wrong activity basis, adding the enzyme too late, using it outside the recommended pH or temperature range, poor mixing, short contact time, or raw-material variation. In troubleshooting, compare actual plant readings with TDS guidance. Check enzyme lot, storage history, addition point, mash profile, wort viscosity, attenuation, and turbidity.
Can the same enzyme program support brewing, winemaking, and distilling?
Some enzyme families overlap across brewing, winemaking, and distilling, but process conditions differ. Substrate, pH, temperature, alcohol level, contact time, and quality targets must be checked for each application. A supplier may offer related enzyme platforms, but each use should have its own TDS review, pilot validation, QC plan, and regulatory suitability assessment.
Related: Brewing enzymes market solutions for clearer, faster production
Turn This Guide Into a Supplier Brief Request a technical consultation, COA/TDS/SDS review, and pilot-trial plan for your brewing enzyme application. See our application page for Brewing enzymes market solutions for clearer, faster production at /applications/brewing-enzymes-market/ for specs, MOQ, and a free 50 g sample.
Contact Us to Contributehello@mail.clearenzyme.com